Where Single Girder Stops and Double Girder Starts
Plenty of plants buy a single-girder crane, run it for three years, and then find it cannot keep up. The load crept up. The shift pattern doubled. Hook height turned out to be short by half a metre. A double girder crane solves all three at once, but it costs more in steel and in building structure, so the decision needs a real reason behind it. This piece covers what a double girder crane actually does differently, the capacity and duty thresholds that force the choice, and how the configuration changes across steel plants, foundries, power stations, cement works and heavy fabrication.
What Makes a Double Girder Crane Different
The structural difference
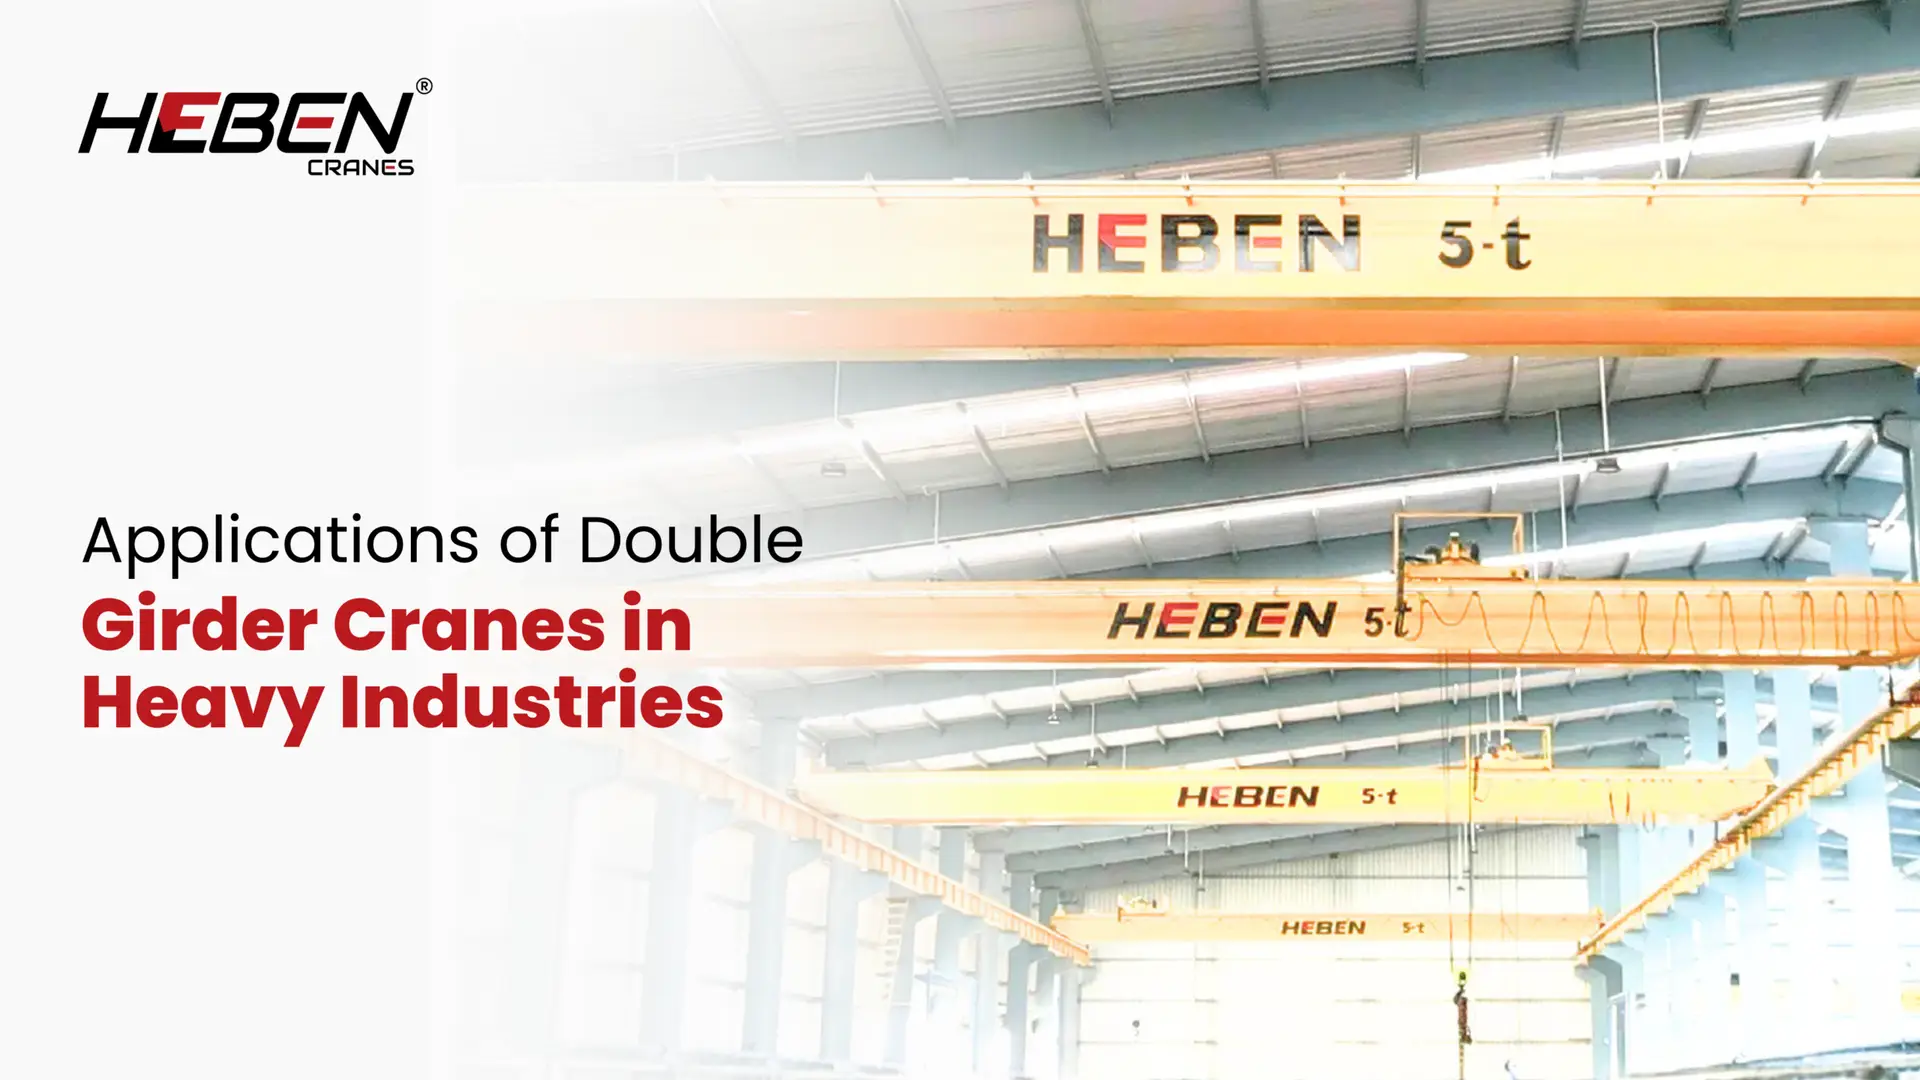
Two bridge beams instead of one, connected to the end carriages at both ends, carrying a trolley that runs on rails laid along the top of the girders. The load path is shared, torsion drops sharply, and the bridge can span further before deflection becomes the limiting factor.
What the top-running trolley buys you
- Hook height. The hoist sits between and above the girders instead of hanging below, which lifts your hook two to three metres higher in the same building.
- Room for attachments. Magnets, grabs, ladle hooks, C-hooks and rotating blocks all need space and cabling that a bottom-running hoist cannot carry.
- A walkway. You can put a maintenance platform along the girder, which turns a shutdown job into a routine one.
- Multiple trolleys. Two trolleys on the same bridge let you turn long loads or share a lift, something no single girder crane can do.
The Thresholds That Force a Double Girder Decision
You are almost certainly in double girder territory once any of these apply:
- Rated capacity above roughly 20 tonnes
- Span beyond 25 metres
- Duty class M6 and above, or continuous multi-shift handling
- Any hot metal, molten material or magnet application
- Hook height that a bottom-running hoist cannot reach in the available headroom
- A need for grabs, ladle attachments, tandem lifting or an operator cabin
Note the pattern: only the first two are about weight. The rest are about what the crane has to do, not how much it has to carry. Many plants specify a double girder crane at 10 tonnes because the duty cycle and the attachment demand it.
Industry Applications
Steel plants and metallurgy
This is the hardest environment a crane works in. Double girder machines handle scrap charging into converters, billet transfer from the caster, coil handling in rolling mills, and finished product stacking. Ambient heat, dust and near-continuous duty push these cranes to the top of the classification range.
Hot metal handling carries its own rulebook. Each hoist unit needs either two holding brakes, each rated at full load hoisting torque, or a single brake rated at 150% of full load hoisting torque. Hoist rope design factor goes to 8:1 against nominal breaking strength, rather than the 5:1 common on general duty cranes. Three wraps of rope must stay on the drum at the lowest hook position.
Foundries and casting shops
Ladle cranes carry molten metal over people and equipment, so redundancy is designed in everywhere — twin drives, twin brakes, backup limit switches, heat-shielded ropes. Mould handling and knockout duties on the same bay usually run a second, lighter trolley on the same bridge.
Power generation
Turbine hall cranes lift generator stators and boiler drums — loads in the hundreds of tonnes that move a few times a year at very slow, very precise speeds. The interesting design tension here is that the crane is rated for enormous capacity but classed for low duty, which changes motor and gearbox selection completely. Micro-speed drives and anti-sway control matter more than travel speed.
Cement and building materials
Kiln shell sections, heavy-duty reducers, clinker grinding mill components. Dust is the defining problem. Enclosed motors, sealed bearings, higher IP-rated panels and frequent filter changes all follow from that.
Heavy machine fabrication
Machine tool beds, pressure vessels, structural assemblies. Double trolley cranes earn their keep here because turning a long weldment safely needs two hooks under coordinated control. Precision positioning matters more than raw speed, which is why variable frequency drives are near-standard.
Ports, warehousing and logistics
Container handling, break-bulk cargo, inland freight stations and large automated warehouses. Long spans, high travel speeds, and duty cycles that run around the clock. Rail wear and wheel maintenance dominate the cost of ownership.
Chemical, paper and hazardous-area plants
Flameproof and explosion-proof double girder cranes for areas with combustible dust or vapour. Every electrical enclosure, motor and light fitting must carry the correct zone certification. Paper mills add roll handling attachments and corrosion protection for humid environments.
Automotive and shipbuilding
Press shop die changes, body-in-white transfer, block turning in shipyards. Automotive plants lean heavily on programmable positioning and interlocks with the production line. Shipyards need long spans and outdoor-grade protection.
Attachments and Configurations for Heavy Duty Work
- Electromagnet: scrap and plate handling. Needs a magnet controller and a backup power supply so the load does not drop on a power failure.
- Grab bucket: bulk material — coal, clinker, ore. Adds a second hoisting motion for open and close.
- Ladle hook: molten metal, with a rotating or tilting block.
- C-hook and coil tongs: steel coils handled on their side.
- Double trolley: long or awkward loads, tandem lifting, or a main and auxiliary hoist arrangement.
- Operator cabin: long spans and high duty, where a pendant operator cannot keep up or cannot see the load.
Getting the Duty Class Right
Duty class is where most specifications go wrong. It is not about capacity — it is about how hard the crane works over its life, combining load spectrum and number of operating cycles.
A crane classed M5 running an M7 workload will not last. Gearboxes and wheels are sized against the class, so under-classing shows up as bearing failure and wheel wear long before anything looks structurally wrong. Count your lifts per hour honestly, estimate the average load as a fraction of rated capacity, and specify from real numbers rather than from what the last crane was.
Features Worth Paying For in a Heavy Industry Crane
- Variable frequency drives on all three motions. Smoother starts, less load swing, far less shock loading on the structure.
- Anti-sway control. Cuts positioning time on long-hook applications and reduces collisions.
- Load monitoring and overload protection. Records actual usage, which turns maintenance planning from guesswork into data.
- Twin drives on long travel. Reduces skewing on wide spans.
- Maintenance walkway and platform access. Pays for itself the first time you avoid hiring a boom lift during a shutdown.
Single Girder vs Double Girder
| Factor | Single Girder | Double Girder |
| Typical capacity | Up to 20 t | 5 t to 500 t and above |
| Span | Up to 25 m | Up to 40 m and beyond |
| Hook height | Lower — hoist hangs below | Higher — hoist sits between girders |
| Duty class | Light to medium | Medium to severe |
| Attachments | Limited | Full range |
| Dead weight and structure cost | Lower | Higher |
| Maintenance access | From below only | Walkway along girder |
FAQs
Can a double girder crane be installed in an existing building? Often yes, but the runway and columns need re-checking against the higher dead weight and wheel loads. In older buildings this frequently means strengthening the runway girders or adding bracing before the crane arrives.
How much extra hook height does a double girder crane actually give? It varies with capacity and hoist type, but two to three metres over a comparable single girder crane in the same bay is typical. On tall loads that difference decides whether the job is possible at all.
Do we need an operator cabin, or is radio control enough? Radio control works well up to moderate spans where the operator can walk with the load and see it clearly. Cabins make sense on long spans, high-temperature areas, continuous duty, and anywhere the floor is too congested to walk safely.
What is the realistic service life of a double girder crane in a steel plant? The structure typically outlives everything else. Expect to replace wheels, ropes and brake components on a cycle measured in years, and to consider a full electrical and drive refit somewhere between year twelve and year twenty depending on duty.
Can we upgrade a double girder crane’s capacity later? Rarely, and not cheaply. The girders, end carriages, wheels and runway are all sized to the original rating. It is much less expensive to specify headroom into the original design than to retrofit it.
Conclusion and Next Step
A double girder crane is not simply a bigger crane. It is a different machine that opens up hook height, attachments, duty class and multi-trolley work that a single girder bridge cannot reach. Match the configuration to the job, class it against real usage, and the crane will outlast most of the plant around it.
About Heben Cranes
Heben Cranes builds double girder EOT cranes for steel, foundry, power, cement and heavy fabrication plants — specified against your duty cycle, your attachments and your building, then installed and load tested on site.
Send us your capacity, span, hook height and shift pattern, and we will come back with a configuration and duty class recommendation. Start the conversation at hebencranes.com.